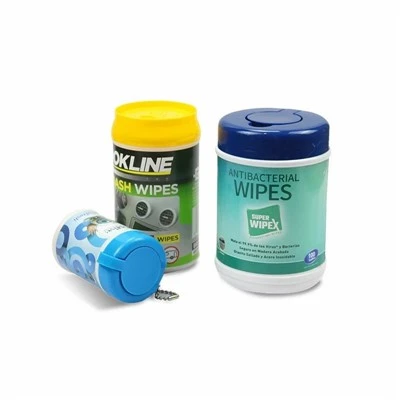

Bag Packed Disinfecting Wipes are professional disposable cleaning wipes engineered for high-efficiency surface hygiene, rapid pathogen reduction, and daily sanitation management. Manufactured within controlled cleanroom facilities utilizing premium-grade nonwoven substrates and advanced antimicrobial or disinfecting liquid solutions, these wipes deliver consistent, reliable performance in eliminating organic soils, stains, and a broad spectrum of microorganisms from high-touch surfaces.
Designed with a robust, resealable closure system, our packaging prevents moisture evaporation and active ingredient degradation throughout extended global logistics, warehouse storage, and daily end-user application. Their lightweight, space-optimized architecture minimizes freight volume and carbon footprint, making them an essential hygiene solution for healthcare environments, commercial office networks, hospitality sectors, educational institutions, and high-traffic public infrastructure.
We specialize in full-scale OEM and ODM manufacturing partnerships for global brand clients, offering end-to-end customization capabilities including proprietary substrate selection, tailored sheet dimensions, customized liquid chemistry profiles, private label artwork execution, and bespoke retail packaging architectures.
Key Features & Professional Technical Advantages
Certified Pathogen Reduction & Efficacy
Our disinfecting formulations are optimized to target and reduce a comprehensive range of bacteria, enveloped viruses, and fungi on frequently touched hard surfaces, supporting rigorous infection control protocols across both institutional and consumer markets.
Rapid Antimicrobial Action: Formulated to achieve effective microbial reduction within short contact times, ensuring immediate surface decontamination in fast-paced commercial settings.
Low-Residue, Streak-Free Chemistry: Engineered with balanced surfactant systems that lift grease and dirt without leaving sticky chemical films or heavy residues on glass, stainless steel, or laminated surfaces.
Regulatory Alignment: Developed in accordance with global biocide and cosmetic safety frameworks, ensuring compatibility with standard international chemical registration requirements (such as EU BPR framework compliance where applicable).
Material-Friendly Profiles: Non-corrosive liquid balances strong cleaning efficacy with material protection, preventing premature degradation of sensitive office hardware, medical cart finishes, and kitchen fixtures.
Premium Nonwoven Substrate Options
Substrate integrity dictates wipe performance. We utilize advanced nonwoven engineering to deliver high tensile strength, optimal fluid retention, and superior release rates.
Available Substrate Classifications:
Spunlace Nonwoven: Composed of high-purity viscose and polyester blends, providing exceptional softness, superior fluid absorption, and high wet-strength for heavy-duty scrubbing.
Airlaid Paper: A cost-effective, highly absorbent matrix ideal for light-duty, high-turnover institutional applications.
100% Biodegradable Plant-Based Substrates: Crafted from certified modal, bamboo, or wood pulp fibers. Designed to disintegrate naturally in municipal composting environments, addressing strict European and North American plastic-free mandates and ESG corporate procurement criteria.
Substrate Performance Metrics: High wet tear resistance prevents fiber shredding during aggressive surface friction; low-linting performance ensures clean application in electronics and healthcare environments.
Advanced Barrier Packaging & Moisture Retention
Global export logistics expose packaging to extreme temperature shifts and humidity gradients. Our pouch architecture prevents premature dry-out and active ingredient breakdown.
High-Barrier Laminate Films: Multi-layer metallic or specialized polymer films block moisture vapor transmission and UV degradation, extending shelf-life beyond 24 months.
Secure Closure Systems: Premium resealable adhesive labels tested for thousands of open-close cycles, alongside optional hard plastic flip-lids that provide an airtight seal to lock in volatile active ingredients.
Logistics Optimization: Compact stackable profiles maximize master carton packing density, lowering international ocean freight and warehousing overhead costs per unit.
Fully Customizable Formulations & Parameters
To match diverse regional regulations and specific brand positioning, our manufacturing lines offer absolute flexibility across all product parameters:
Custom Sheet Counts: Scalable packaging formats ranging from 10-count pocket travel packs to 120-count high-capacity household or professional dispensers.
Liquid Chemistry Adaptability: Options include alcohol-based (isopropanol or ethanol blends for rapid evaporation) and alcohol-free, quaternary ammonium-based or plant-derived surfactant formulations.
Sensory Profiles: Fragrance-free options for sensitive healthcare environments, alongside micro-encapsulated fresh, lemon, or botanical scents that leave a clean olfactory impression without overwhelming indoor air quality.
Technical Specifications Matrix
|
Specification Parameter |
Manufacturing Options & Engineering Limits |
|
Product Classification |
Bag Packed Disinfecting and Sanitizing Wipes |
|
Primary Substrate Materials |
Spunlace Nonwoven (Viscose/Polyester), Airlaid Paper, 100% Biodegradable Plant Fibers |
|
Substrate Basis Weight |
40 GSM to 80 GSM (Customizable based on durability requirements) |
|
Substrate Color |
Optic White or Custom-Dyed Ecological Tints |
|
Wipe Dimensions |
Customized (e.g., $15 \times 20\text{ cm}$, $18 \times 20\text{ cm}$, $20 \times 20\text{ cm}$, up to $25 \times 30\text{ cm}$) |
|
Sheet Count per Unit |
10 to 120 Sheets per Resealable Pouch |
|
Primary Packaging Material |
Multi-Layer High-Barrier PET/PE or PET/ALU/PE Film Structures |
|
Closure Mechanism |
Resealable Sticky Label with Optional Hard Plastic Flip-Lid |
|
Liquid Formula Matrix |
Broad-Spectrum Disinfecting Solution (Alcohol-Based or Alcohol-Free Options) |
|
Fragrance Profiles |
Fragrance-Free, Fresh, Citrus Lemon, Mild Botanical, Custom Scents |
|
Target End-Use Applications |
Institutional Surface Disinfection, Commercial Facility Maintenance, Consumer Hygiene |
|
Manufacturing Quality Standards |
Produced in ISO 22716 and GMP Certified Cleanroom Facilities |
|
OEM / ODM Support |
Full Private Label, Custom Packaging Design, and Regulatory Dossier Support |
Target Applications & Industrial Sectors
Commercial Enterprise & Corporate Facilities: High-frequency disinfection of shared office workstations, conference room touchpoints, shared keyboards, door handles, and elevator buttons to support employee health and safety guidelines.
Hospitality & Food Service Networks: Front-of-house dining table sanitization, guest room touchpoint maintenance, and back-of-house surface hygiene management requiring fast turnover and safe chemical profiles.
Healthcare & Institutional Environments: Routine auxiliary surface cleaning in clinics, dental offices, assisted living facilities, and educational campus classrooms where infection prevention is paramount.
Retail & Public Transit Infrastructure: High-turnover consumer hygiene distributions, airport terminal seating sanitation, and public mobility vehicle interior maintenance.
Why Global Procurement Leaders Choose Our Manufacturing Partnership
Verified Compliance and Cleanroom Manufacturing Excellence
Procuring disinfecting wipes for Western markets requires absolute assurance of facility hygiene and regulatory compliance. Our production operations are executed within certified cleanroom environments adhering to ISO 22716 (Cosmetic and Hygiene Good Manufacturing Practices) and GMP standards. This ensures every production batch maintains rigorous microbiological control, preventing cross-contamination and assuring brand owners of uncompromised product safety.
Comprehensive R&D and Regulatory Integration
Navigating international chemical regulations (such as strict biocidal product regulations in Europe or EPA compliance guidelines in North America) can delay market entry. Our internal chemistry and regulatory teams assist global buyers with formula optimization, safety data sheet (SDS) compilation, and efficacy testing documentation to align seamlessly with destination-market legal frameworks.
Bulletproof Quality Control (QC) Protocols
To safeguard your brand reputation and eliminate costly international return liabilities, we enforce a strict multi-stage quality assurance protocol:
Raw Material Verification: Tensile strength testing, fiber purity checks, and heavy metal screening for all incoming nonwoven rolls.
In-Process Chemical Monitoring: Automated titration and pH checks during liquid impregnation to guarantee uniform active ingredient saturation across every batch.
Packaging Integrity Inspection: Vacuum decay and dye-penetration seal testing to verify pouch hermeticity, ensuring zero dry-out risk during lengthy maritime transit.
Final Pre-Shipment Audit: Random sampling conducted according to international acceptance quality limit (AQL 1.0 / 4.0) standards before container release.
FAQ
Hot Tags: bag packed disinfecting wipes, China bag packed disinfecting wipes manufacturers, suppliers, factory, Multi-Surface Antibacterial Disinfecting Wipes, 80 Count